REFERENCE REPORT
ALLIED PRINTING
Key Facts About Project
Company: Allied Printing Services, Inc.
Location: Manchester, Connecticut, USA
Industry: Commercial Printingmerlin®
Solution: merlin® ALPHA high-pressure humidification system & RO Box 6 water treatment
Target relative humidity: 50%
Benefits: reduced static electricity, improved productivity
In operation since: January 2025
INDUSTRIAL HUMIDIFICATION IN COMMERCIAL PRINTING
Allied Printing Services, Inc. – Stable Production Through Controlled Humidity by Merlin Technology Inc.
Initial Situation: Static Electricity as a Production Risk
During the winter months, significantly reduced humidity levels led to severe static electricity issues. These impacts extended across the production workflow including printing, finishing, and trim collection.
Static discharge caused disruptions, reduced process stability, and negatively impacted overall production efficiency. For a high-performance commercial printing company, these issues not only increased operational risk but also limited productivity during critical periods.
Requirements: Reliable Humidity Control Across the Entire Facility
Allied Printing Services sought a professional solution to maintain stable and consistent humidity levels throughout the production, storage, and warehouse environments
The humidification requirements were defined around two key priorities.
Functionality: The system needed to maintain a consistent relative humidity level of 50% across all designated areas, which would result in a reduction of static electricity, minimize press downtime, and improve overall production throughput.
Reliability: System must be a turnkey solution, designed for dependable, low-maintenance operation in the background, allowing the production team to remain focused on core manufacturing activities.
The Solution: merlin® ALPHA System with integrated Water Treatment
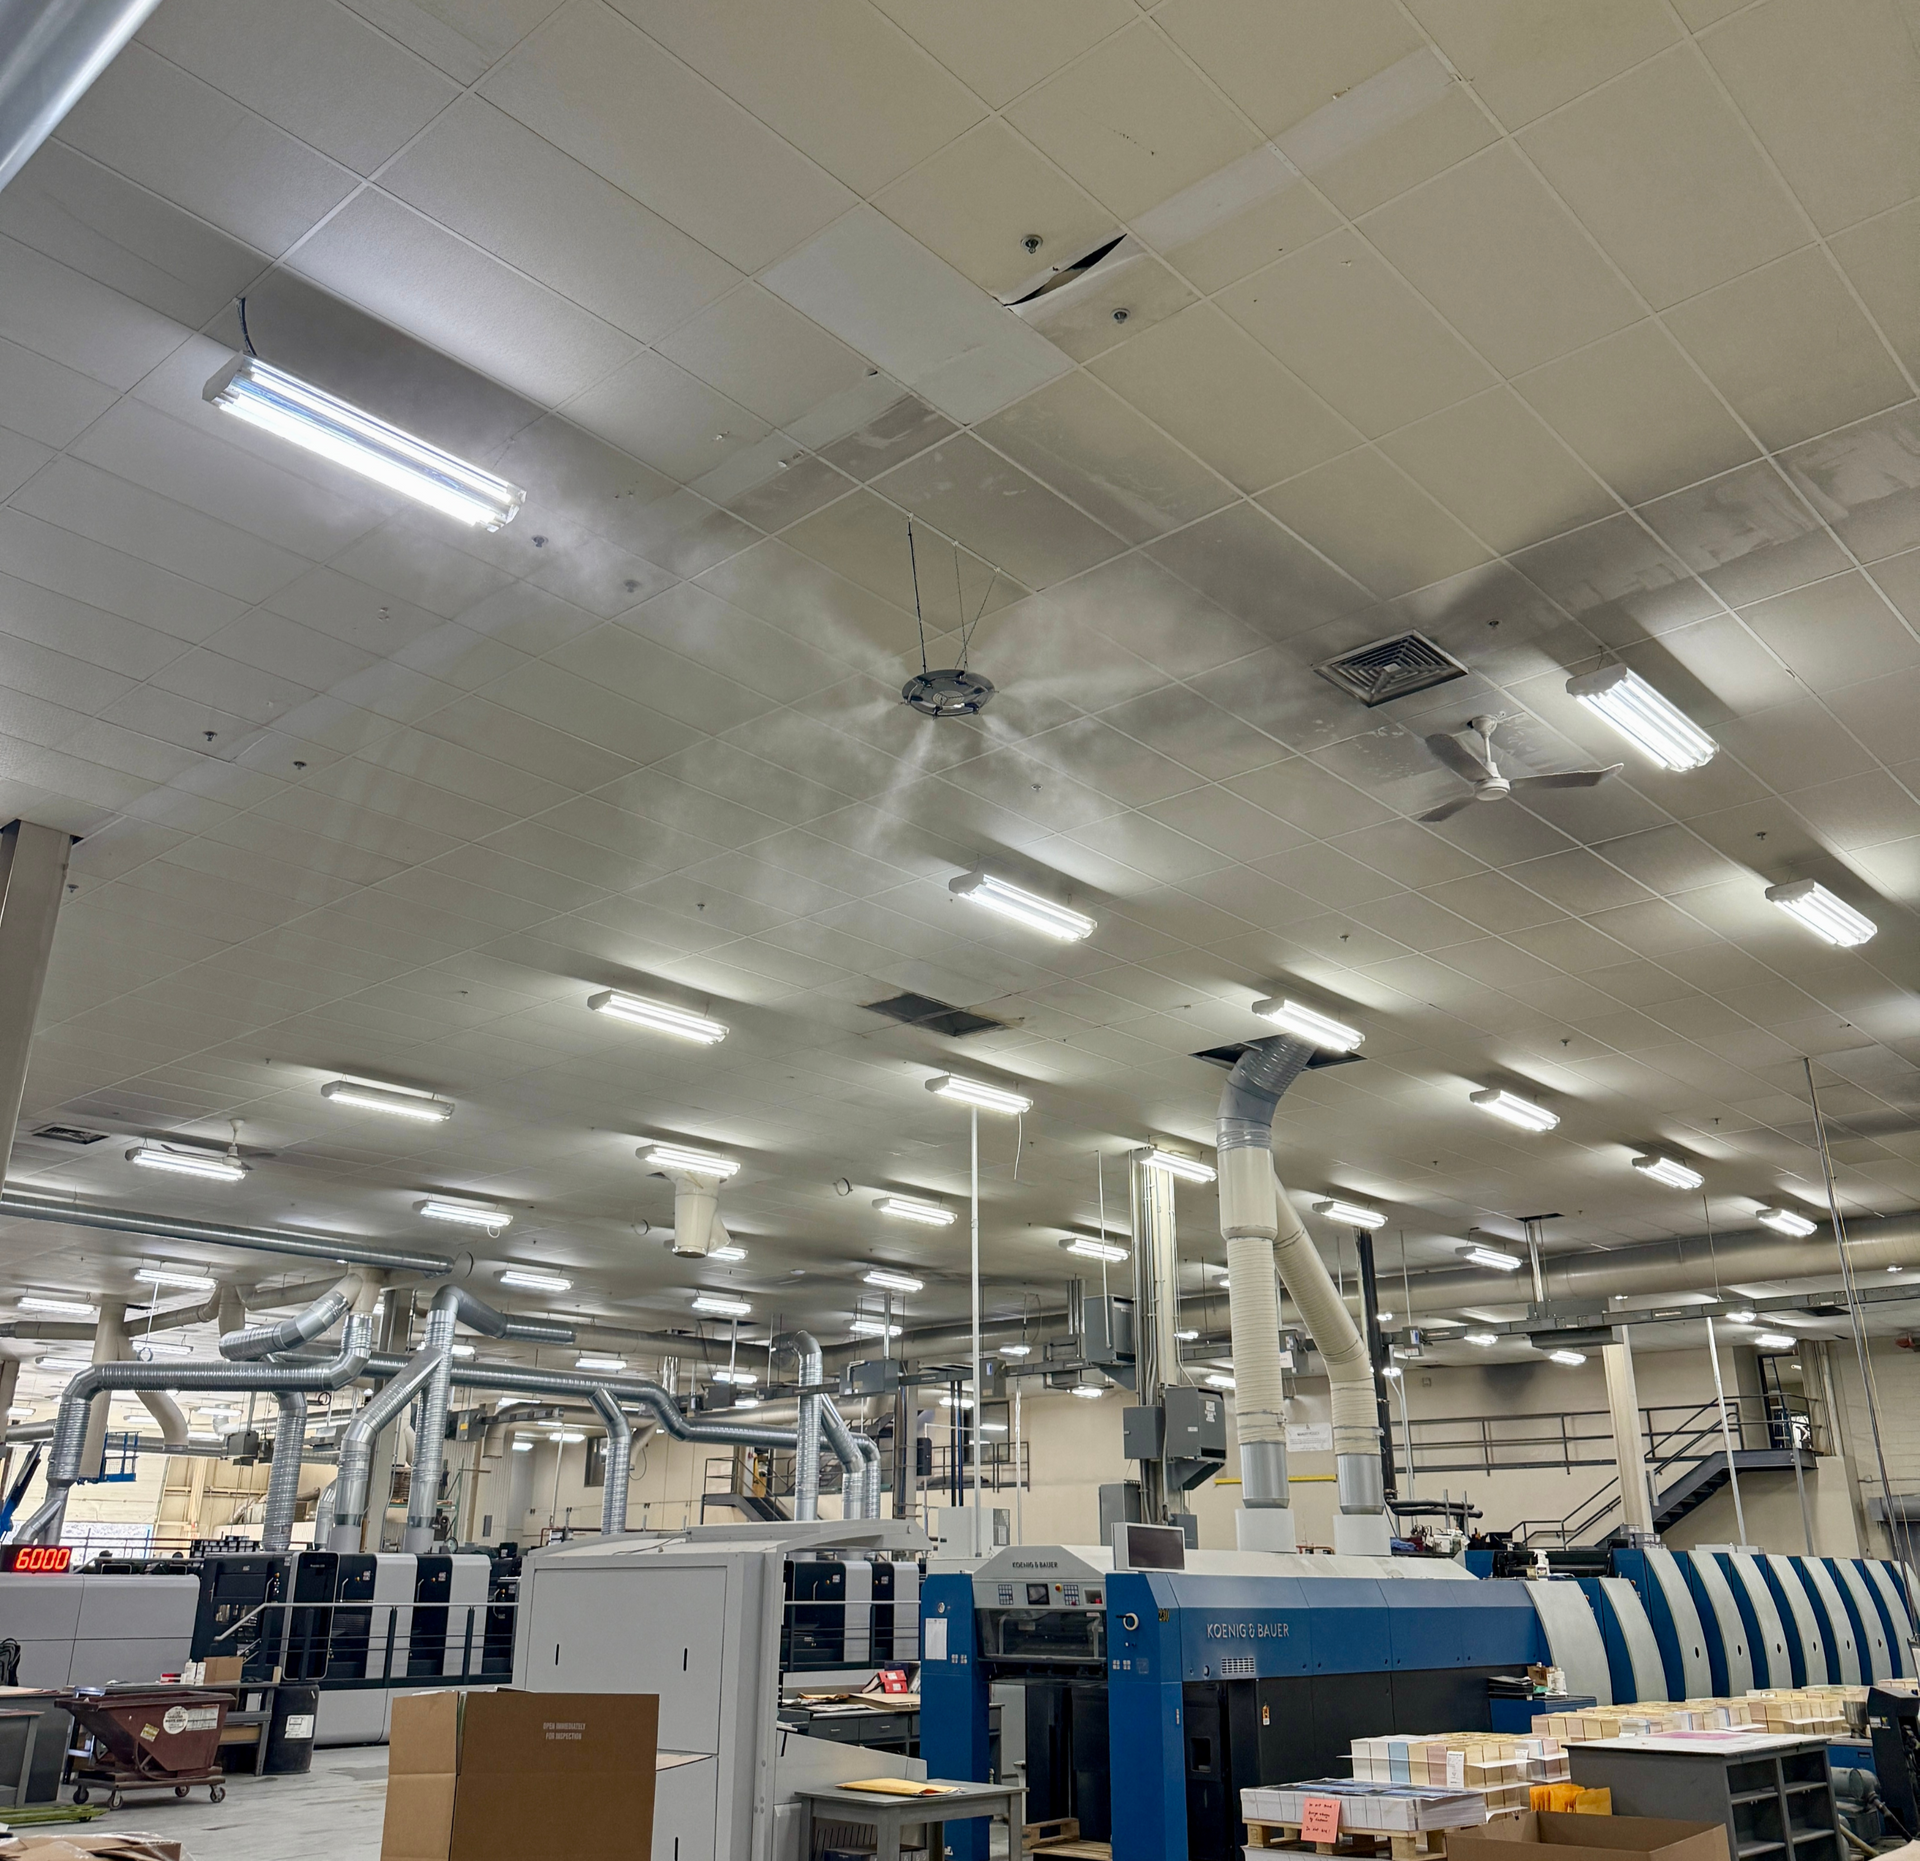
Allied Printing Services selected merlin® Technology to design and implement a custom humidification solution tailored to the specific requirements of their facility. A fully engineered system utilizing the ALPHA adiabatic high-pressure platform was developed, featuring an 8-zone configuration to enable precise and flexible humidity control across various production areas. Each zone can be independently adjusted to meet distinct environmental conditions within the facility.
The merlin® Alpha system incorporates a maintenance-free, water-lubricated variable frequency drive (VFD) pump, designed to deliver reliable and efficient operation. The PLC-based control system forms the core of the solution, managing the water treatment process, monitoring humidity levels, and coordinating the operation of each zone’s humidification equipment.
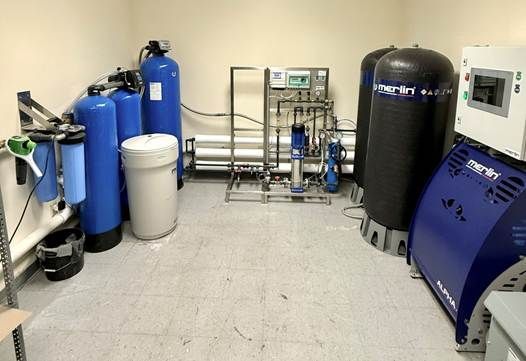
The reverse osmosis (RO) system plays a critical role in ensuring water quality by effectively removing minerals from the municipal water supply. Designed with a capacity of 395 gallons per hour (gph), the system achieves up to 99.5% reduction of dissolved minerals and bacteria.
To support optimal performance, the RO system is complemented by a comprehensive pretreatment process. This includes pre-filtration to eliminate suspended particles, a water softener to reduce hardness, and an activated carbon filter to remove chlorine—protecting the RO membranes from degradation.
This integrated approach ensures consistent water quality while promoting long-term system reliability and operational stability.
Results: Higher Efficiency and Improved Process Stability
Since the installation of the merlin® system, Allied Printing Services has maintained stable relative humidity levels in the 50% range throughout the facility. Static electricity has been significantly reduced across all key production areas.
As a result, workflows have become more consistent—particularly in finishing and trim collection—leading to improved overall process stability. The reduction in static-related disruptions has directly enhanced productivity and supported more reliable print operations, especially during the dry winter months.
Customer Feedback: Service and Support That Stand Out
In addition to the technical performance of the system, Allied Printing Services highlights the quality of support provided by merlin®:
“The technical support and service personnel from merlin® are second to none."
— Chris Gouveia, Senior Vice President / General Manager, Allied Printing Services, Inc.
Added Value for Commercial Printing Companies
This project highlights the impact of targeted industrial humidification in optimizing printing and finishing operations. By reducing static electricity, the system enhances production efficiency, ensures smoother material handling, and maintains stable operating conditions. As a result, product quality remains consistent across all stages of production.
For commercial printers facing similar challenges, controlled humidification represents a critical component in achieving reliable operations, improved efficiency, and consistent output quality.
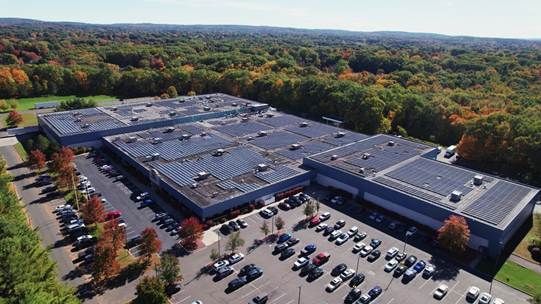
Production facility of Allied Printing Services in Connecticut, USA